

Worker safety holds a paramount place in industrial manufacturing operations for several reasons: primarily because protecting the well-being and health of employees is the right thing to do. Beyond that, regulatory requirements have strict workplace safety standards, and a track record of unsafe practices can result in punishments including fines and even shutdowns. Unsafe facilities will also find it more difficult to attract skilled workers and are likely to see their reputation and business suffer as well.
Industry 4.0 technology and other innovations today are making a major positive impact on workplace safety in manufacturing and maintenance, whether directly or indirectly. Read on to learn how these technologies are working to improve workplace safety for all involved.
1. IIoT & Device Infrastructure
The Industrial Internet of Things is a set of technologies, hardware and infrastructure that enables the smart factory of today: connected, data-driven and focused on operational efficiency and continuous improvement. IIoT technology and the connected infrastructure of sensors, monitors and communications technology are behind safety improvements in maintenance and inspection, helping to detect potential equipment problems before they lead to the kinds of catastrophic failures that can put operators and other personnel at risk. In addition, industrial monitors can reduce or eliminate the need for hands-on equipment monitoring and inspection that can often prove dangerous.
2. Condition-based monitoring
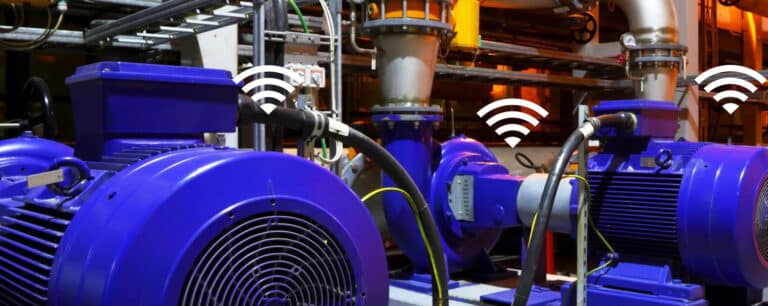
Industrial sensors, along with communications technology, form the backbone of the smart factory, also known as the connected factory. Sensor technology plays a major role in machine health monitoring, which helps to enable real-time, remote monitoring that facilitates predictive maintenance—an approach that proactively monitors the condition of machines to identify potential abnormalities in key performance indicators to fix them before a breakdown and unplanned downtime can occur.
3. Wearable technology
Wearable safety technology for manufacturing represents some of the most promising safety improvement ideas in manufacturing, facilitating individual safety while also collecting data to enable safer conditions throughout the facility. On the personal safety front, wearables can detect motion, falls, positioning, shocks and vibration, as well as heart rate and other biometric indicators. Wearable detectors for gas, temperature, moisture and other conditions can also provide early detection of problem states, alerting both the wearer and the wider facility of the need to relocate and address workplace hazards. Sensors worn on the body also detect if workers come too close to moving machinery and alert them so they can take appropriate action in hazardous environments. In addition, wearables like goggles can provide heads-up displays and visualizations that can help with enhancing workplace safety, as described in further detail in the next section.
4. Augmented & virtual reality
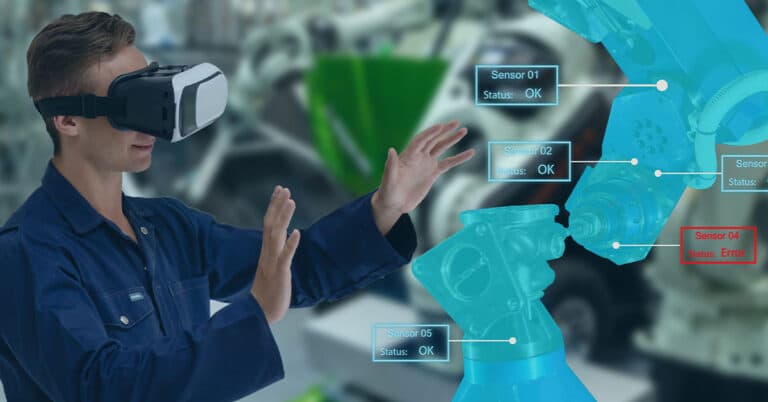
Wearable goggles are among the most commonly used Industry 4.0 technologies in manufacturing, facilitating more accurate and effective maintenance, faster training (including safety training programs), and AR and VR in manufacturing. AR and VR have significant safety implications in manufacturing, as they are able to replicate actual parts and objects, including their current conditions, in virtual space through digital twin and similar technologies. This technology enables technicians to troubleshoot maintenance issues without the need to disassemble equipment, which can lead to incidental or more serious workplace injuries.
5. Artificial intelligence
Artificial intelligence is among the most exciting new workplace safety technology in manufacturing, with the ability to make improvements in numerous areas across maintenance and production. These include:
- Improved, earlier identification of maintenance failure states
- Identification of different types of failure states
- Assistance in troubleshooting maintenance issues without the need to disassemble equipment
Machine learning algorithms featuring AI also can analyze workplace safety incident records and detect patterns that can be used to guide decisions surrounding scheduling to reduce safety risks. Modern AI systems have been deployed that can use machine vision to check for employees wearing proper personal protective equipment and provide alerts when the right protective gear is not detected.
6. Robotics
Robotics have long formed the underpinnings of automation technology, and this field continues to advance today. Much of today’s robotics technology is a far cry from the legacy automation equipment that must be partitioned off from personnel for safety purposes—collaborative robots, or cobots, are designed to work directly alongside human workers, increasing productivity, enabling more innovation in production processes, and increasing safety throughout the facility thanks to failsafe and other “smart” technology that automatically stops processes if potential risks are detected.
7. Mobile applications
Mobile applications enable remote, real-time monitoring and alerting of environmental factors such as gas, temperature, chemicals and more. With mobile technology, the right personnel can be notified immediately, no matter where they are, if processes need to be shut down or personnel relocated from the facility.
8. Drones
Drone technology enables a number of safety improvements throughout manufacturing facilities, including “birds-eye” monitoring throughout the facility, with the ability to visually detect potential problems as well as the ability to use onboard sensors to monitor gas, temperature and chemical levels; access to dangerous areas of the facility for monitoring, troubleshooting and more; and pick-and-place and transportation of messages or items throughout the facility, which can reduce repetitive injuries and provide help to workers in dangerous scenarios.
As you can see, much of the technology driving advances in Industry 4.0 has the added benefit of safety improvements for workers throughout the facility. With increased connectivity and assistance from this technology, today’s manufacturing workers are safer than ever. However, it’s also critical that manufacturers commit to building a culture of safety that holds every worker responsible for maintaining a safe workplace. Technology is an important tool, but it cannot be seen as a substitute for a vigilant and mindful workforce.
Contact us to learn more about our safety and technology-driven predictive maintenance solutions. Interested in downloading this content? Get the infographic.